You have no items in your shopping cart.
Global buyers are seeking lighter frames, cleaner sightlines, and efficient material use. Slim Profile Aluminum extrusions answer these needs in doors, lighting systems, display fixtures, solar equipment, and compact machinery. Their narrow geometry can improve visual appeal without sacrificing practical strength.
The International Aluminium Institute reports that global primary aluminium production reached approximately 70.6 million tonnes in 2023. Its technical guidance also notes that recycled aluminium requires about 5% of the energy used for primary production. These figures make alloy selection, recycled content, and supplier traceability important purchasing factors. The International Energy Agency further identifies aluminium as an energy-intensive material requiring deeper efficiency and decarbonisation efforts. Better design matters.
This guide examines top slim-profile options for international buyers. It considers common alloys, wall thickness, dimensional tolerance, surface finishing, load requirements, and production capability. Alloy 6063 remains widely used for architectural applications because it offers good extrudability and attractive anodized finishes. Alloy 6061 may suit applications requiring higher mechanical strength, although it can be less convenient for complex profiles.
A thin wall is not automatically a better wall. It may complicate tooling, packing, machining, or installation. Buyers should request mill certificates, inspection records, finish samples, and clear tolerance data before approval. Standards such as EN 755, EN 12020, and ASTM B221 can support consistent evaluation, depending on the project region.
The selection process is rarely perfect. Supplier claims may sound precise, yet practical performance depends on design details and handling conditions. This overview combines published industry evidence with buyer-focused experience, while recognising that local codes and project specifications must still control final decisions.
Top Slim Profile Aluminum Extrusions for Global Buyers
What Defines a Slim Profile Aluminum Extrusion?
A slim profile aluminum extrusion is defined by proportion, not appearance alone. Designers usually assess the outer envelope, wall thickness, weight, and bending stiffness together. Many compact profiles use walls around 1.5 to 2.0 millimeters, but this range is not a universal standard. A 20-millimeter frame can be slim for lighting, yet unsuitable for a loaded machine guard. The boundary is not perfectly standardized.
In practice, one recurring mistake is choosing the narrowest section before checking deflection. A slim profile should still provide enough moment of inertia for its span and load. Engineers should review alloy temper, corner radii, screw channels, and extrusion tolerances. The Aluminum Association’s Aluminum Standards and Data publication remains a useful reference for alloy and temper selection. Manufacturing limits matter too. Extremely thin walls can increase die complexity, distortion, and surface variation.
Material efficiency also supports global procurement decisions. The International Aluminium Institute reports that recycled aluminum requires about 5% of the energy used for primary aluminum production. Its sector outlook also indicates strong demand growth through 2050. Therefore, buyers should request recycled-content evidence, dimensional inspection records, and lifecycle documentation. A lighter profile is not automatically a better profile. Sometimes, it is simply under-designed. Careful testing beats attractive catalog dimensions.
Slim profile aluminum extrusions help create clean edges without making frames visually dominant. Their narrow sightlines can bring more glass into a window or display assembly, while consistent profiles support a considered, repeatable design. That matters in retail fronts, interior partitions, and compact enclosures. Details show. A recessed channel can conceal fasteners, and a carefully sized groove can accept a gasket or panel edge. Still, a thinner profile is not automatically a better one; load, span, and connection details need checking before dimensions are fixed.
Performance depends on the whole assembly, not appearance alone. Aluminum is light for its strength and resists corrosion in many common environments, but its high thermal conductivity can transfer heat across a frame. Where insulation matters, thermal breaks and suitable glazing may be necessary. For installation, accurately cut lengths, deburred ends, and compatible corner connectors reduce awkward adjustments on site. A sample corner is worth assembling before a full order. It can reveal a tight gasket or a fastener that sits proud. Slim profiles may also leave less room for wiring and hardware, a limitation that is easy to overlook on a screen. Planning those clearances early makes fitting more predictable, though real site conditions can still demand small changes.
Aluminum has an approximate density of 2,700 kg/m³, compared with about 7,850 kg/m³ for steel and 8,960 kg/m³ for copper. Its lower density can help reduce component and assembly weight, while the final result depends on the alloy, profile geometry, and application.
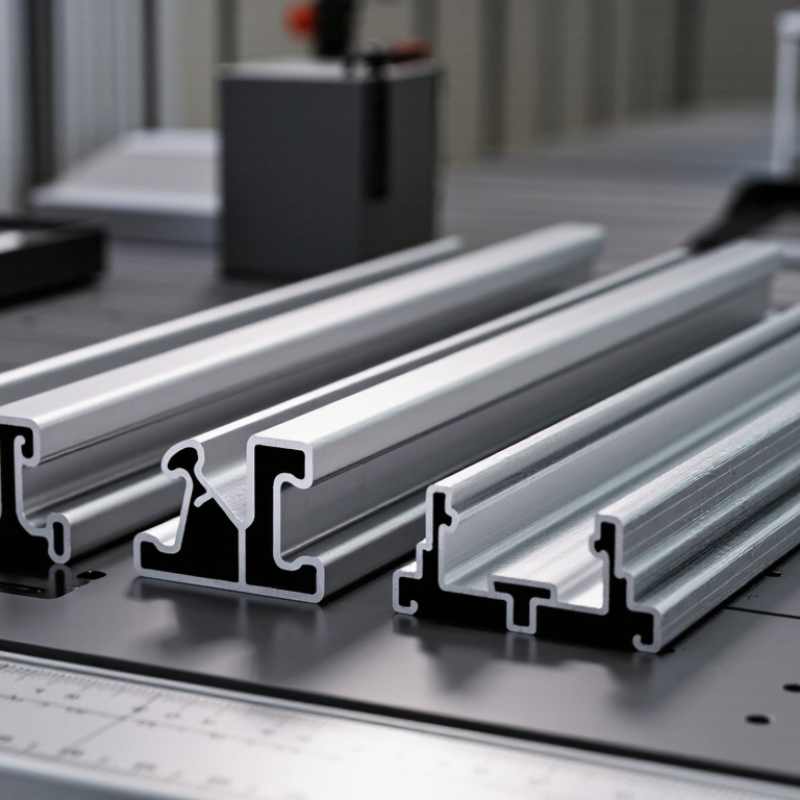
Slim aluminum extrusions commonly use narrow U-channels, T-slots, flat bars, and hollow sections.
Each shape solves a different problem: a slim U-channel can hide wiring, while a thin-walled rectangular tube adds stiffness without much bulk. Alloy choice matters. 6063 is widely used for architectural profiles and smooth finishes; 6061 offers higher strength for load-bearing components, though its surface appearance may be less refined.
The International Aluminium Institute’s 2020 report projected global aluminum demand could rise by nearly 40% by 2030. That growth makes careful material selection more important, not less.
Finish affects both appearance and service life. Mill finish is economical but shows handling marks; anodizing creates a durable oxide layer, while powder coating adds color and surface protection.
For coastal or frequently cleaned installations, ask suppliers about finish thickness and corrosion testing. Small details count.
Customization can include tighter dimensional tolerances, mounting slots, drilled holes, or cut-to-length pieces. Yet very slim walls can complicate extrusion and raise the risk of distortion.
A practical drawing should state wall thickness, alloy, temper, finish, and critical dimensions.
One detail buyers sometimes overlook: the proposed profile should be reviewed against the extrusion press and die limits before tooling is approved. I have seen attractive designs need revision at this stage.
Top Slim Profile Aluminum Extrusions for Global Buyers
How to Select the Right Extrusion for Global Projects
Selecting a slim aluminum extrusion starts with the project’s actual load, span, and installation method. In project reviews, I have seen buyers choose by appearance alone. That approach often creates deflection, weak joints, or difficult assembly. Request the alloy, temper, wall thickness, and dimensional tolerances before comparing prices. These details affect strength, machinability, and long-term stability.
Check the profile against real operating conditions. A narrow channel may suit a lightweight display frame but fail in a vibrating machine enclosure. Consider fastener access, cable routing, drainage, and room for thermal movement. A small change in wall thickness can alter weight and stiffness significantly. Ask for section properties and load calculations when the extrusion supports equipment or panels. Do not rely only on a catalogue image.
Surface finish also matters for international projects. Anodizing can improve appearance and surface durability, while powder coating offers broader color options. Confirm coating thickness, color references, packing methods, and inspection records. I once underestimated packaging space, and shipping damage followed. The profile was correct; the delivery plan was not. Request production samples, tolerance reports, and clear drawings in agreed units. Metric dimensions reduce confusion, but conversion errors still happen. Build time for testing, revisions, and local assembly practices. A technically suitable extrusion may still need adjustment after the first prototype.
Use this guide to compare common slim-profile extrusion types. Dimensions and wall thickness are project-specific rather than universal; confirm the final design, tolerances, alloy, temper, and applicable local requirements with the extrusion supplier and project engineer.
| Profile Type | Common Alloy and Temper | Key Selection Factors | Typical Applications | Global Project Checks |
|---|---|---|---|---|
| Slim architectural frame | 6063-T5 or 6063-T6 | Visible face width, glazing or panel fit, corner joints, surface finish, and required stiffness. | Windows, doors, partitions, display frames, and interior systems. | Confirm dimensions and tolerances against the project specification. Check relevant building, glazing, and safety requirements for the installation market. |
| Light structural profile | 6061-T6 or 6005A-T6 | Applied loads, unsupported length, deflection, connection design, and resistance to local buckling. | Equipment frames, supports, transport components, and lightweight structures. | Have the section and connections checked for the actual design loads. Do not select a profile by appearance or alloy designation alone. |
| Compact heat-sink profile | 6063-T5, 6063-T6, or 6061-T6 | Available space, base thickness, fin geometry, airflow, heat load, and mounting method. | LED assemblies, power electronics, and other thermal-management equipment. | Validate thermal performance in the intended operating conditions. Confirm machining, coating, and interface requirements before production. |
| Slim LED channel | Commonly 6063-series alloy | LED strip width, diffuser fit, heat dissipation, end-cap fit, and mounting clearance. | Linear lighting, cabinet lighting, and architectural lighting details. | Check the complete assembly, including diffuser material, electrical components, and any applicable regional lighting or electrical requirements. |
| Modular T-slot profile | Commonly 6063-T5 or 6063-T6 | Slot dimensions, fastener compatibility, joint strength, frame deflection, and accessory availability. | Machine guards, workstations, automation frames, and modular fixtures. | Verify slot geometry and accessory compatibility across the supply chain; similar-looking profiles may not share the same slot dimensions. |
| Slim glazing or panel rail | Commonly 6063-series alloy | Panel thickness, gasket design, drainage, fixing method, and wind or service loads. | Lightweight glazing assemblies, screens, and façade or interior panel systems. | Confirm system-level performance, including water management, structural support, and local code requirements; profile selection alone does not establish compliance. |
Specification note: Aluminum alloy properties depend on alloy, temper, product form, and applicable standard. For international purchasing, state the required alloy and temper, drawing units, dimensional tolerances, finish, inspection criteria, and governing standard in the purchase specification. Standards such as ASTM B221 and EN 755-9 address aluminum extrusion products and dimensional tolerances; confirm the applicable edition and requirements for the project.
Slim-profile aluminum extrusions require more than attractive dimensions. Alloy selection, wall thickness, straightness, and surface consistency affect performance. The International Aluminium Institute reported about 70.6 million tonnes of global primary aluminum production in 2023. That scale creates choices, but not every supplier controls extrusion quality equally. Request mill certificates, alloy verification, dimensional inspection, and coating test results. Standards such as EN 755, ASTM B221, and ISO 9001 can support evaluation. However, a certificate alone does not prove every batch.
Sourcing should include realistic tolerances, minimum order quantities, tooling ownership, and production lead times. Ask for sample pieces before approving a full run. Check thin walls carefully; small bends may appear after cutting or packing. This is where experience matters. I would also inspect corner radii and anodized color under consistent lighting. Color matching is often less perfect than catalog images suggest. That detail deserves attention.
Tips: Compare at least three suppliers using the same technical drawing. Confirm packaging before production. Foam separators, capped ends, and reinforced cartons can prevent scratches and deformation. For international shipping, plan around container space, moisture protection, customs documents, and correct tariff classification. UNCTAD states that maritime transport carries over 80% of global merchandise trade, so port delays can affect even small extrusion orders. The World Bank’s 2023 Logistics Performance Index also highlights customs efficiency and shipment reliability as major logistics factors. Build buffer time. Freight estimates can be optimistic.