You have no items in your shopping cart.
In 2026, print manufacturers face tighter quality demands, shorter runs, and rising material costs. The right Inspection Machine For Printing can protect brand consistency before defective rolls reach customers. Yet “best” does not mean the fastest camera or the highest price. It means matching inspection accuracy, web speed, lighting, software, and operator skill to the production line. A converter producing flexible packaging needs different controls from a label printer or a commercial press. That difference matters.
A practical evaluation should begin with real samples, not a polished brochure. Test registration shifts, pinholes, color variation, streaks, missing print, and splice defects at normal production speed. Ask vendors to demonstrate detection results on difficult substrates, including reflective film and textured paper. Check how the system records images, marks defects, and integrates with rewinding or slitting equipment. Industry experience shows that clear alarms and simple review screens often save more time than impressive specifications. Small details count.
This guide compares leading inspection approaches for 2026 through measurable criteria. These include resolution, false rejects, inspection width, data security, service response, and total ownership cost. It also considers training, calibration, and maintenance over several years. No machine performs perfectly in every condition. Dust, vibration, changing inks, and poor lighting can expose weaknesses. A careful buyer should request site trials and documented performance data. Some preferences may need reconsideration. The strongest choice is the system that detects meaningful defects consistently, supports operators, and proves its value on your own press.
In 2026, the best printing inspection machine depends on the press, substrate, and defect risk. A narrow web label line needs different control from a large sheet-fed press. In production trials, I have found that inspection accuracy starts with stable lighting, clean reference files, and correct camera alignment. No system is perfect.
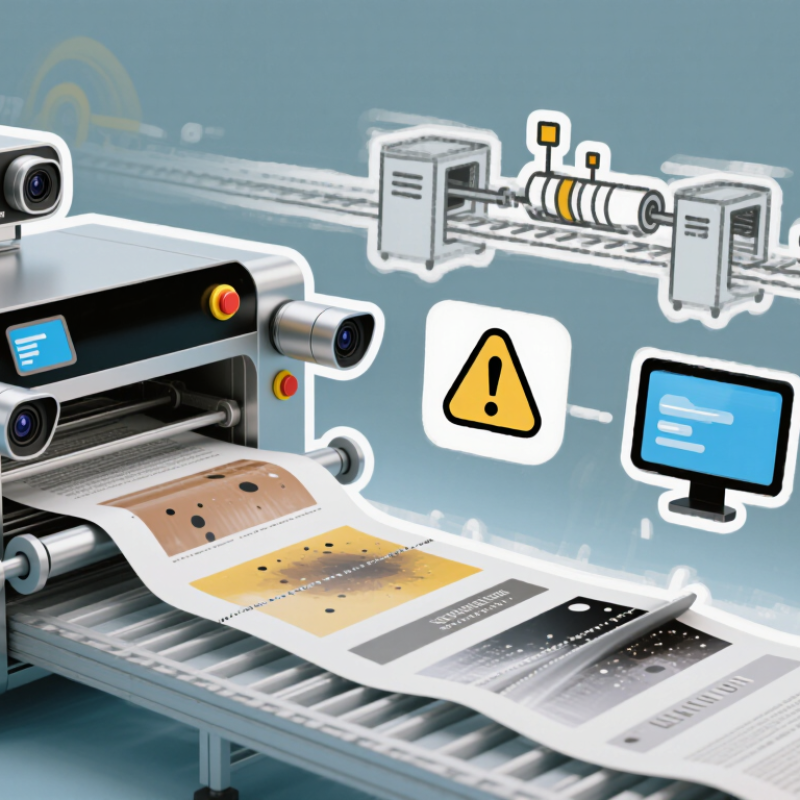
Web inspection machines monitor continuous rolls while printing. They detect missing text, streaks, pinholes, color shifts, and registration errors at high speed. Sheet-fed vision systems inspect each printed sheet and can track defects by sheet number. This helps operators remove faulty sheets before packing. Print quality inspection systems compare live images with approved samples. They measure contrast, density, sharpness, and fine details. Color measurement modules add objective data when visual checks become inconsistent.
Variable-data inspection machines read barcodes, QR codes, serial numbers, and changing text. They are useful for packaging, tickets, and personalized documents. Some systems combine these functions with AI-assisted defect classification. That feature can reduce false alarms, but it still needs careful setup. In my experience, reflective films and textured paper often confuse cameras. Manual samples remain valuable.
The right choice should match line speed, resolution, inspection width, and required traceability. A practical evaluation uses real production materials, including dark ink, metallic areas, wrinkles, and small text. Operators should test changeover time as well. A technically powerful machine may perform poorly when its settings are difficult to adjust. Human review still matters.
Modern print inspection systems combine high-resolution cameras, LED lighting, artificial intelligence, and precise software controls. These technologies inspect every label, carton, or flexible package while the web moves at production speed. The best machine is not simply the fastest one. It must detect practical defects without creating excessive false rejects.
Line-scan cameras remain essential for continuous web inspection. They capture narrow image strips and build a complete picture across the moving substrate. Multispectral lighting can reveal missing ink, color variation, scuffing, and contamination. AI-based classification then separates serious defects from harmless paper texture. According to the 2024 drupa Global Trends report, more than 500 printing companies and suppliers reported continuing pressure to improve efficiency and automation. That pressure makes real-time inspection increasingly valuable.
Data connectivity also matters. Modern systems can link inspection results with production records, color measurements, and waste reports. Smithers’ market analysis identifies automation and digital quality control as major influences on printing’s future development. In practice, a useful system should store defect images, locate faults accurately, and support quick operator decisions. Not every AI alert is correct. Poor lighting, reflective film, and changing substrates can confuse detection software. Human review still matters, especially during setup and unusual jobs. The strongest choice is therefore a balanced system with reliable cameras, adaptable algorithms, clear reporting, and simple maintenance.
The best inspection machine is not always the fastest one. Compare performance under real production conditions, not only showroom demonstrations. Measure inspection speed at your normal web width, material thickness, and ink coverage. A machine that reaches high speed with clean samples may struggle with dense graphics or reflective film.
Start with detection accuracy. Test small pinholes, missing print, color variation, streaks, and registration shifts. Record both missed defects and false alarms. Too many false alarms can slow operators and create unnecessary waste. Ask for repeatability data across several production runs. One successful trial proves very little.
Image resolution matters, but lighting design matters just as much. Uneven illumination can hide defects near edges or dark backgrounds. Check how the system handles dust, vibration, splices, and changing roll tension. Review its data tools too. Useful reports should show defect location, size, time, and production conditions. Integration with rewinding equipment can save hours, but only if the signals remain reliable.
Operators should adjust settings without complicated procedures. Maintenance access deserves attention. A camera that takes half a day to clean may reduce practical uptime. I would also compare training time, service response, and spare-part availability. No scorecard is perfect. My own mistake was judging a system by detection rate alone. Total performance includes stable operation, usable data, and fewer interruptions. Test the machine with your hardest production job before making a final decision.
What Is the Best Inspection Machine for Printing in 2026?
Best Machine Features for Different Printing Applications
In 2026, the best inspection machine depends on the printing application, not only camera resolution. A narrow web label line needs fast color registration checks, barcode reading, and splice detection. Small defects matter. A system should also store defect images beside the production record. This helps operators verify problems instead of relying on memory.
Folding carton production requires stable sheet handling and precise print-to-cut registration. Look for cameras that inspect fine text, missing varnish, ink smears, and die-cut edges. For flexible packaging, glare control is essential. Reflective films can hide pinholes or weak seals under ordinary lighting. Multi-angle illumination and adjustable exposure can reveal these defects more consistently.
Commercial printing benefits from variable-data verification, especially for serialized pages, addresses, and security patterns. High-speed line-scan cameras work well on continuous webs, while area-scan cameras may suit slower sheet-fed presses. Textile printing needs broader coverage and image comparison across repeating patterns. In real production, setup time matters as much as detection accuracy. A powerful system can still fail when operators avoid complicated menus.
Machine learning can reduce false alarms, but it should not replace experienced review. Some acceptable texture variations may look defective to software. Testing with real materials, production speeds, ink densities, and intentional sample defects is more reliable than trusting a showroom demonstration. I would also check lighting maintenance, calibration steps, data export options, and service response times. These details seem ordinary. They often decide whether inspection becomes dependable or frustrating.
| Printing Application | Recommended Inspection Machine | Typical Substrates | Inspection Method | Typical Camera Resolution | Typical Line Speed | Key Defects Detected | Best Machine Features | Main Selection Consideration |
|---|---|---|---|---|---|---|---|---|
| Flexible Packaging | 100% web inspection system with line-scan cameras | Plastic film, laminated film, foil, coated paper | Continuous optical inspection with reference-image comparison | 2,048–8,192 pixels per line | 150–600 m/min | Missing print, color variation, streaks, pinholes, registration errors, wrinkles and splices | High-speed line-scan imaging, strobing illumination, automatic defect classification and roll mapping | Match camera resolution and lighting to the smallest defect that must be detected without reducing production speed |
| Labels and Narrow-Web Printing | Compact 100% inspection system with high-magnification imaging | Paper labels, synthetic labels, transparent films and self-adhesive stock | Web inspection combined with print-to-print registration checking | 2,048–4,096 pixels per line | 30–180 m/min | Unreadable text, barcode defects, missing characters, color shifts, die-cut errors and substrate contamination | High optical magnification, barcode and OCR verification, fast job changeover and low-waste setup | Choose software that supports variable artwork, multiple SKUs and reliable barcode grading |
| Commercial Sheetfed Printing | Sheet inspection system with front-and-back camera modules | Coated paper, uncoated paper, board and specialty sheets | Sheet-by-sheet inspection against a digital or approved reference image | 100–300 dpi at the sheet level | 8,000–18,000 sheets/hour | Set-off, hickeys, ink spots, scumming, missing images, smearing and misregister | Stable sheet transport, synchronized LED lighting, front/back inspection and automatic sheet marking | Mechanical stability and precise sheet tracking are essential for dependable detection at high delivery speeds |
| Folding Cartons and Paperboard Packaging | High-resolution flat-sheet inspection system with color measurement | Folding carton board, solid bleached board and recycled board | Full-sheet visual inspection with color and geometric verification | 150–400 dpi at the sheet level | 6,000–15,000 sheets/hour | Print defects, color drift, barcode errors, missing varnish, coating defects and incorrect artwork | Large field of view, color consistency monitoring, barcode verification and defect location reporting | Use a system that separates acceptable process variation from defects that affect packaging function or compliance |
| Rotogravure Printing | High-speed web inspection system with synchronized illumination | Flexible films, foil, paper and laminated webs | Continuous optical inspection synchronized with the gravure press | 2,048–8,192 pixels per line | 250–800 m/min | Doctor-blade lines, hickeys, voids, ink splashes, pinholes, color variation and cylinder-related repeat defects | High dynamic range, repeat-defect analysis, defect trend monitoring and automatic roll classification | Lighting must reveal low-contrast defects while avoiding glare from transparent or metallized materials |
| Flexographic Printing | Web inspection system with registration and density monitoring | Films, paper, corrugated liner, foil and pressure-sensitive stock | Line-scan inspection with color-density and register analysis | 2,048–8,192 pixels per line | 150–600 m/min | Plate damage, dirty print, ink starvation, slur, dot gain, missing print and color-to-color misregister | Multi-channel lighting, repeat-length analysis, automatic splice detection and production trend alarms | Prioritize fast response to recurring defects so operators can correct the press before large amounts of waste are produced |
| Corrugated Board Printing | Large-format inspection system designed for uneven surfaces | Corrugated liner, single-wall board and double-wall board | Area-scan or line-scan inspection with surface-tolerant imaging | 100–250 dpi at the board level | 4,000–12,000 sheets/hour | Missing print, crushed areas, ink smears, warped board, poor registration and incorrect graphics | Wide field of view, depth-of-field tolerance, dust-resistant housing and robust sheet tracking | Optical performance should be validated on the actual flute profile and board grade used in production |
| Security and Document Printing | High-resolution inspection system with multi-spectral imaging | Security paper, banknotes, certificates, identity documents and controlled forms | Multi-spectral image comparison with feature and sequence verification | 300–1,200 dpi equivalent detail inspection | 30–300 m/min | Missing security elements, incorrect numbering, fine-line breaks, registration errors and unauthorized variations | UV or infrared illumination options, secure audit trails, serial-number verification and restricted data access | Data security, traceability and controlled recipe management are as important as optical resolution |
| Digital Printing | Variable-data inspection system with file-based verification | Paper, labels, films, envelopes, cartons and specialty media | Printed-image comparison against the intended variable-data file | 300–1,200 dpi equivalent detail inspection | 30–150 m/min | Wrong text, missing variable data, banding, nozzle lines, color inconsistency and image distortion | Job-data integration, OCR, barcode validation, page sequencing and automatic reject control | Integration with the digital front end and production database is critical for preventing mix-ups between jobs |
| Pharmaceutical and Medical Packaging | Validated vision inspection system with serialization support | Paper cartons, labels, foil blisters and coated packaging materials | 100% print, code and package-feature inspection with electronic records | 300–600 dpi equivalent detail inspection | 60–400 packs/min | Unreadable batch codes, incorrect expiry dates, missing text, barcode failures and artwork mismatches | OCR and OCV, code grading, reject confirmation, user access control and complete inspection records | Select equipment that supports documented validation, audit trails and controlled recipe changes |
| Newspaper and High-Volume Editorial Printing | High-throughput web inspection system optimized for process defects | Newsprint, lightweight coated paper and recycled paper | Continuous grayscale or color web inspection | 1,024–4,096 pixels per line | 300–900 m/min | Web breaks, ink density variation, missing pages, set-off, streaks and registration errors | Very high scanning speed, low-light operation, automatic defect alarms and waste reduction analytics | System uptime, easy operator response and reliable detection at high web speeds usually outweigh extreme resolution |
| Finishing and Post-Press Verification | Inline or offline vision inspection system for assembled products | Folded cartons, booklets, brochures, labels and bound products | Image comparison, sequence checking and dimensional inspection | 200–600 dpi equivalent detail inspection | 2,000–20,000 products/hour | Wrong page sequence, missing inserts, folding errors, damaged edges, incorrect gluing and mixed products | Product tracking, reject verification, dimensional measurement and batch-level reporting | Inspection should be synchronized with the finishing line to prevent good products from being rejected or defective products from passing |
In 2026, the best printing inspection machine is not simply the fastest model. It is the system that detects meaningful defects without slowing production. Selection should begin with the print process. Define the substrate, maximum web width, line speed, ink structure, and smallest defect that matters. A narrow label line needs different optics from a wide flexible packaging line. Request tested samples, not only catalog figures. Real trials reveal performance under glare, dust, contrast changes, and registration shifts.
Image resolution requires careful attention. Higher resolution can expose pinholes, missing text, and color variation, but it may increase data load and false alarms. Stable lighting is equally important. Compare reflection control, camera exposure, and calibration routines during a live trial.
The software should classify defects clearly, save inspection images, and trace rolls by time or job number. Operators need readable alerts. Complicated screens create avoidable mistakes. Check encoder compatibility, reject signals, network security, and press-control integration.
Reliability comes from repeatable results, not a polished demonstration. Request uptime records, maintenance intervals, training plans, and response procedures. Verify recipe changes between short jobs. Ask how inspection data is stored and accessed. No machine is perfect. Advanced systems may confuse metallic ink with a defect or miss flaws outside the camera view. That weakness should be documented. An acceptance test should include known defects, clean samples, speed changes, and deliberate lighting variation. Feature lists look impressive, but daily consistency matters more.